
Fiber Cement Board Production Line Commissioning: From Installed Machines to the First Accepted Board

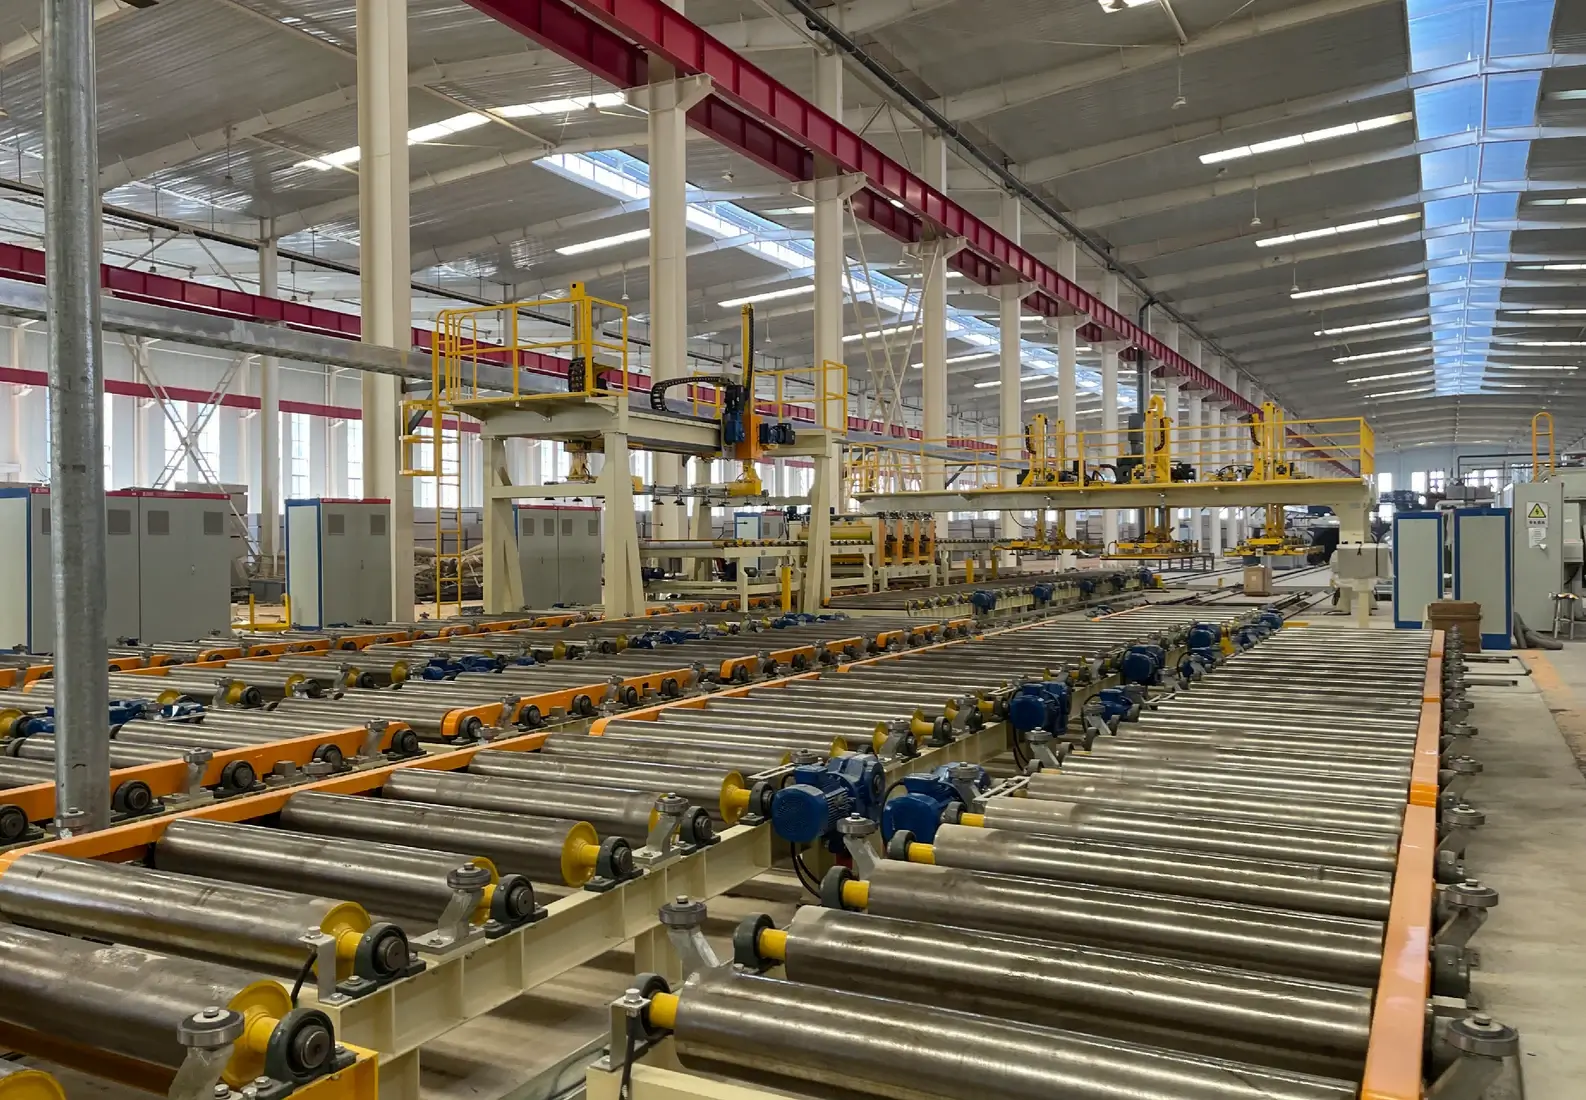
Fiber Cement Board Production Line Commissioning is complete only when the installed machinery can produce an agreed board through a repeatable sequence and the operating team understands how to run and maintain that process. Mechanical erection alone does not prove this result. A factory can have correctly installed equipment and still experience unstable slurry preparation, damaged green sheets, curing-load delays or unacceptable final dimensions. Before site acceptance begins, the owner and engineering supplier should agree the launch product, trial materials, machinery scope, utilities, tests and responsibilities for correcting issues. Zhonghong describes process engineering, machinery manufacturing, electrical automation, delivery, installation, commissioning, operator training and production support. Its equipment range covers raw-material preparation, forming, cutting, stacking, selected pressing and stripping, autoclave curing, splitting and finishing. The commissioning plan should follow that actual installed sequence rather than a generic checklist copied from another factory.
An investor starting a new production plant may have never operated this process before. A factory replacing only its forming section may have experienced staff and existing equipment that must remain in service. The first project needs to establish a complete working production method; the second needs to demonstrate that the new station does not disrupt a proven material flow. These are different commissioning scopes even if both are described as a production-line start-up.
Before the first slurry batch, confirm what installation has actually delivered
Site teams should distinguish machinery installation from process operation. A fabrication or factory acceptance test may have verified the supplied machine’s assembly and selected functions before shipment. After installation, the team must check the actual connections, protective systems, machine movement and interfaces to adjacent stations. The responsible engineers should decide which tests can be performed without production material and which require the intended board.
Equipment identity, foundations and services must match approved drawings
Zhonghong’s Ball Mill, Automatic Dosing System, Slurry Storage Tank and forming equipment have different mechanical and utility needs. The installation team should verify that the machines delivered correspond to the approved schedule and that their actual connections are consistent with the plant design. Foundation requirements, process piping and power or steam services should come from the offered equipment, not from an unrelated factory illustration.
A new-plant investor should also know which site work was supplied by the owner and which by the engineering provider. A retrofit team needs to confirm how retained machines connect to new assemblies. If that division remains unclear, the first process trial may be delayed by missing services or mismatched transfer heights even though every purchased machine arrived on time.
Electrical checks should precede integrated material movement
Zhonghong offers Electrical Control Cabinets and an Intelligent Line Control System that links PLC control with production monitoring. The commissioning team should verify the functions actually included, the machine states and relevant safety provisions before running an integrated line. IEC 60204-1 provides general requirements for electrical equipment of machines; it does not certify a particular supplier’s installation without appropriate evidence and assessment.
Make the first production trial a test of prepared material, not only the former
The wet end depends on acceptable raw materials and an operating feed route. A Ball Mill may prepare mineral inputs where required, Automatic Dosing measures formula ingredients, and a Slurry Storage Tank supplies prepared material to the chosen forming system. Commissioning should identify the approved recipe and the state of material needed at each transition. The site cannot reasonably claim a finished-board result if no suitable formulation or feed material has been agreed.
A dosing record must correspond to the batch actually released
During trial production, the process team should know which product is being made and what material has entered the system. The Automatic Dosing System’s function is to meter the ingredients of an approved formulation, but correct metering does not guarantee suitable raw-material characteristics. If a batch differs from expectations, the team should determine whether the issue belongs to the feed, preparation, measurement or process conditions rather than changing the forming machine indiscriminately.
Consider a factory whose test batch is made using a different local mineral source from the sample used during equipment design. The commissioning plan should account for material characterization and any necessary formulation trials. A machine supplier cannot turn an unverified feedstock into a guaranteed board by adjusting a generic setting. The agreement needs to state who provides samples, performs process development and approves the first material batch for forming.
Hatschek and Flow-on forming require distinct operating observations
The company’s Hatschek Forming Machine builds a wet sheet through multiple cylinders and layer accumulation. Its Flow-on Forming Machine uses slurry distribution, dewatering and thickness control. An operator should understand which route is installed, what the machine receives and how the resulting wet sheet is evaluated. A demonstration of one forming method should not be represented as the commissioning procedure for the other without project-specific evidence.
Zhonghong’s Thickness Measurement System displays board thickness during forming. That observation can support process evaluation, but it does not establish automatic control or final-board compliance by itself. The operations team should identify the wet measurement target for the agreed product and where finished thickness will later be inspected. If deviations occur, recording when they first appear can help avoid arbitrary adjustments to unrelated stations.

The first green sheet must pass cutting, stacking and transfer without damage
Producing a visually plausible sheet at the former is not the end of wet-end commissioning. Zhonghong’s high-pressure Waterjet Cutting System sizes green boards, and its servo-controlled Board Stacker positions them for the next operation. Depending on the product, a Hydraulic Press or Stripping Machine may also be included. The trial should follow actual material across each required station and record which machine is responsible for the handoff.
Cut-to-stack trials reveal weaknesses that empty-machine tests miss
An empty cutter and stacker can both move correctly while the actual green board is poorly supported between them. The commissioning team should test with the agreed product dimensions and material condition. The operator needs to see when a cut is complete, how a sheet is transferred and what constitutes a successfully prepared stack. A trial at only one easy size should not be used to claim that every proposed future format is already qualified.
Suppose the factory plans a later variant with longer boards. It can include that product as a separate trial when the material is ready, but the first objective should be a repeatable commercial launch board. This helps the plant resolve support and transfer issues before complexity from several sizes is added. A claimed equipment speed is not useful if boards cannot consistently arrive at the receiving station in acceptable condition.
Controlled stops should be tested without improvising an unsafe restart
A trial should include the agreed response when the Board Stacker cannot discharge a load or a downstream conveyor is unavailable. The controls supplier should describe which upstream movements are inhibited, what operators observe and which conditions permit the line to resume. These events must be planned and risk-assessed by responsible personnel; they are not instructions to bypass protective functions or test dangerous failures casually.
Curing-area trials need real loads and the approved board process
For applicable fiber-cement and calcium-silicate products, Zhonghong offers an Autoclave Curing System. The selected process and load arrangement must be developed against the material and board to be made. An autoclave requires suitable site services, protective systems and qualified operating procedures. Commissioning its mechanical or pressure equipment is not the same as proving the finished product meets a relevant construction-material specification.
Loading, treatment and unloading are separate milestones
A Board Stacker may prepare material for treatment, while a Shuttle Car transfers appropriate trolleys into or around the curing area. The autoclave performs the treatment, and the Board Splitter separates cured sheets from supports afterward. These functions should be demonstrated as a connected route where included. The supplier should explain the actual load plan, movement sequence and equipment interfaces, rather than assume a vessel’s nominal size proves factory throughput.
A factory whose loads are delayed at the receiving station may not need another curing vessel. During commissioning, operators can observe whether treatment or handling is the real constraint. No universal steam temperature, pressure, cycle time or load capacity has been published for every Zhonghong project, so those values must come from the validated process and ordered equipment. They should not be improvised during start-up or borrowed from another manufacturer’s brochure.
Pressure-equipment checks and finished-sheet tests have different authorities
The applicable pressure equipment and site-safety rules depend on the installed system and destination. Qualified specialists must determine the required inspections and operating approvals. A finished fiber-cement board may separately need product testing under a relevant standard such as EN 12467 where applicable. Neither kind of evidence substitutes for the other. The plant commissioning file should record the machine and product results as distinct milestones.

Finished-board inspection is where an equipment start-up becomes a product trial
After curing, the factory may use a Board Splitter, Sanding Machine, Grinding & Chamfering Machine and Board Cutting Machine depending on its commercial product. These are distinct functions. Commissioning should verify each operation against what the board needs, including dimensions, surface or edge acceptance and transfer into the following station. An equipment package that runs automatically can still produce a board the market will not accept if those criteria were never defined.
The first accepted sheet should be traceable to the process used
A useful trial record can identify the intended board, raw-material assumptions, forming route, handling stages and finished-product measurements. It should also distinguish equipment checks from board acceptance. If a defect appears, the factory can then determine when it developed rather than treat every rejection as a final cutter problem. The level of recording should be agreed for the project; the public site does not establish any mandatory proprietary tracking database.
An architectural-facing board may require particular surface and edge conditions, while an interior substrate can have different priorities. The commissioning plan should match the actual sales specification and the appropriate tests, not a generic description of high quality. If a later product needs additional sanding or a different cut, that new configuration should be evaluated separately rather than assumed accepted through the first trial.
Operator training must be tied to the installed line, not a general presentation
Production staff should understand the machine states, product-specific settings, inspection points and appropriate procedures for maintenance or process interruptions. Zhonghong lists installation, training and production support in its engineering offering, but the contract must identify what the customer receives. Training on actual machines with the intended product is more useful than a presentation that describes equipment without its site interfaces.
Handover should close the questions that held up the first production run
Before accepting commissioning, the buyer should identify what was demonstrated, what issues remain open and who is responsible for the next action. Factory acceptance, installed machinery checks, product trials and routine operation are related but not interchangeable. A well-managed project uses separate evidence for each so that equipment suppliers and the factory owner can agree what has actually been achieved.
A clear completion record prevents the same interface dispute returning
If the waterjet cutter and stacker required a control modification, the handover should identify which change was made and what test confirmed it. If the autoclave loading route was changed, its revised movement sequence should be documented. If the first board formulation required trial adjustments, the approved product conditions should be kept available for the operating team. That record is more valuable than an unqualified statement that the entire factory now runs perfectly.
The plant planning article connects equipment choices to the intended board, while the production bottleneck guide distinguishes brownfield commissioning from new-factory start-up. Zhonghong’s company engineering description provides the broader supply and support context. The actual acceptance schedule must still name the machines and tests relevant to the specific contract.
Stable production is a verified condition, not a slogan
The owner should be able to follow its first approved commercial board from material preparation to finished inspection and show that operators understand the process. That does not mean every future grade, speed or annual capacity is automatically guaranteed; later changes need their own engineering and testing basis. It means the accepted product and its operating route have been demonstrated within the scope that the parties agreed.
Successful commissioning gives the factory a reproducible starting point and a useful technical record. The buyer can accept equipment whose functions were actually tested, recognize any unverified assumptions and operate the line without relying on a generic promise of turnkey success. That is the practical standard by which a fiber-cement board production project should be handed over.